High-precision mobile diagnostic hardware and treatment systems engineered for institutional performance.

How evolving healthcare workflows are driving the design requirements of next-generation surgical, anesthetic, and utility medical carts.
Integrated with advanced antimicrobial surface coatings, high-grade polymer structural layers, and gapless welding designs that prevent pathogenic cultivation and survive aggressive chemical washdowns.
Seamless support for integrated power modules, high-capacity battery solutions for uninterruptible operations, and micro-motion pneumatic height adjustment for clinician physical well-being.
Interchangeable drawer systems, high-capacity medication compartments, standard accessory mounting rails, and reliable locking configurations for customized clinical needs.
In modern critical care environments, the medical trolley is no longer just a static platform for storage. It has evolved into a key element of point-of-care workflows. Modern hospitals require high-mobility cart systems that can securely support medical equipment, interventional instruments, and medication distribution panels. According to industry analyses, the market for smart clinical utility carts is growing due to the expansion of telemedicine, digital health records, and the necessity of immediate access to specialized tools in high-pressure medical environments.
Purchasing managers from healthcare groups, primary care hospitals, and medical research institutes emphasize safety and longevity. Carts must withstand repeated disinfection with harsh reagents (e.g., sodium hypochlorite, isopropyl alcohol) without physical degradation. They must also maintain clean surfaces to reduce the risk of healthcare-associated infections (HAIs).
The manufacturing of premium medical trolleys requires a precise combination of materials. ABS (Acrylonitrile Butadiene Styrene) polymers are utilized for worktops and drawer covers due to their chemical resistance, impact absorption, and ease of cleaning. Meanwhile, high-grade structural alloys, such as T6 series aviation-grade aluminum and SUS304 stainless steel, provide the internal strength and rigid foundation needed to prevent twisting under heavy loads.
Furthermore, medical castors require high-performance, non-marking polyurethane or synthetic rubber with precision sealed ball bearings. This ensures silent operation in recovery wards and easy maneuverability around tight corners in emergency rooms. Dynamic testing protocols, including ramp tests and obstacle course evaluations, are critical to ensuring safe movement during rapid emergency responses.
Qingdao MDV Medical Appliances Co., Ltd. is a modern enterprise focusing on the R&D, manufacturing, and sales of anesthetic medical products, traditional Chinese medicine acupuncture, interventional products, injection puncture, and nursing medical equipment. The company has passed the ISO 13485 Medical Device Quality System Certification.
We focus on high-quality medical equipment, patient care, and providing reliable products and services. We continuously upgrade our existing product lines and develop new solutions. With numerous patented products, we meet the demand for specialized medical equipment worldwide.
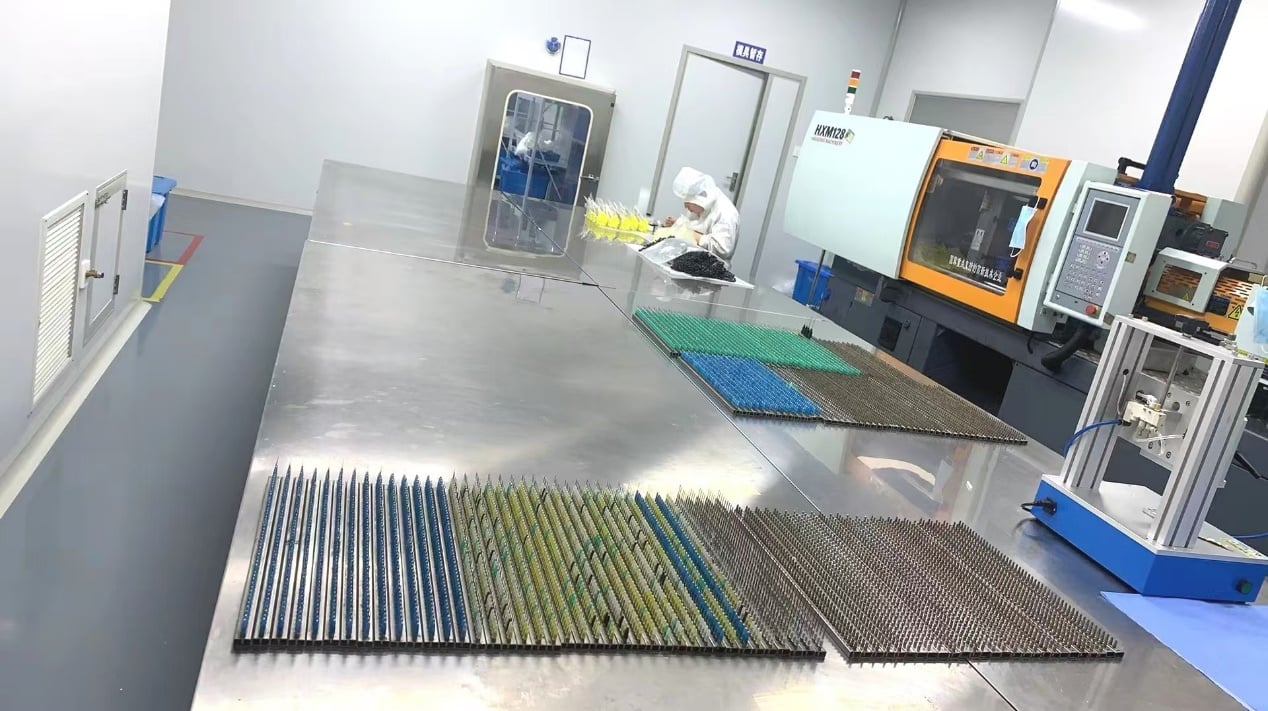
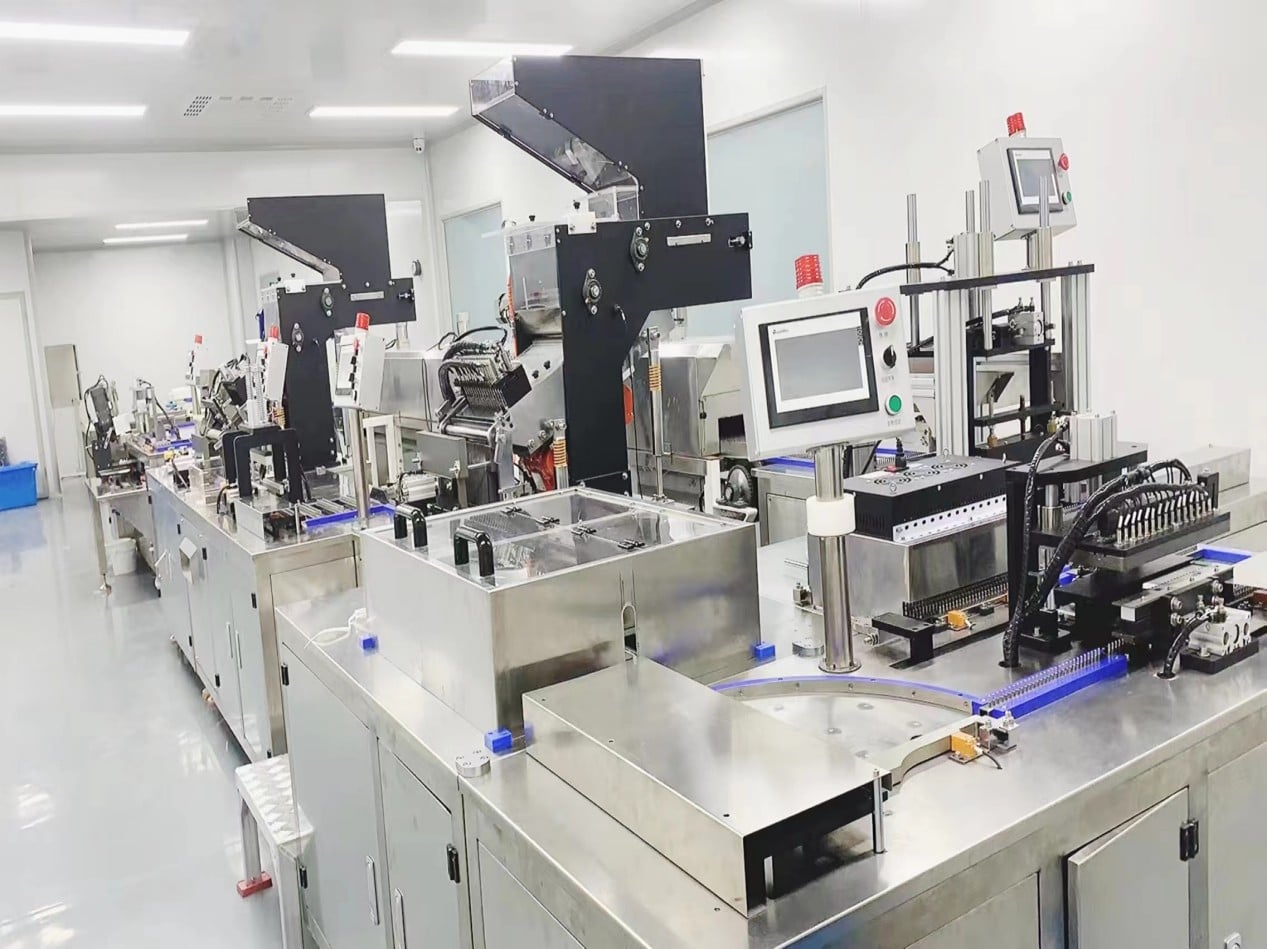
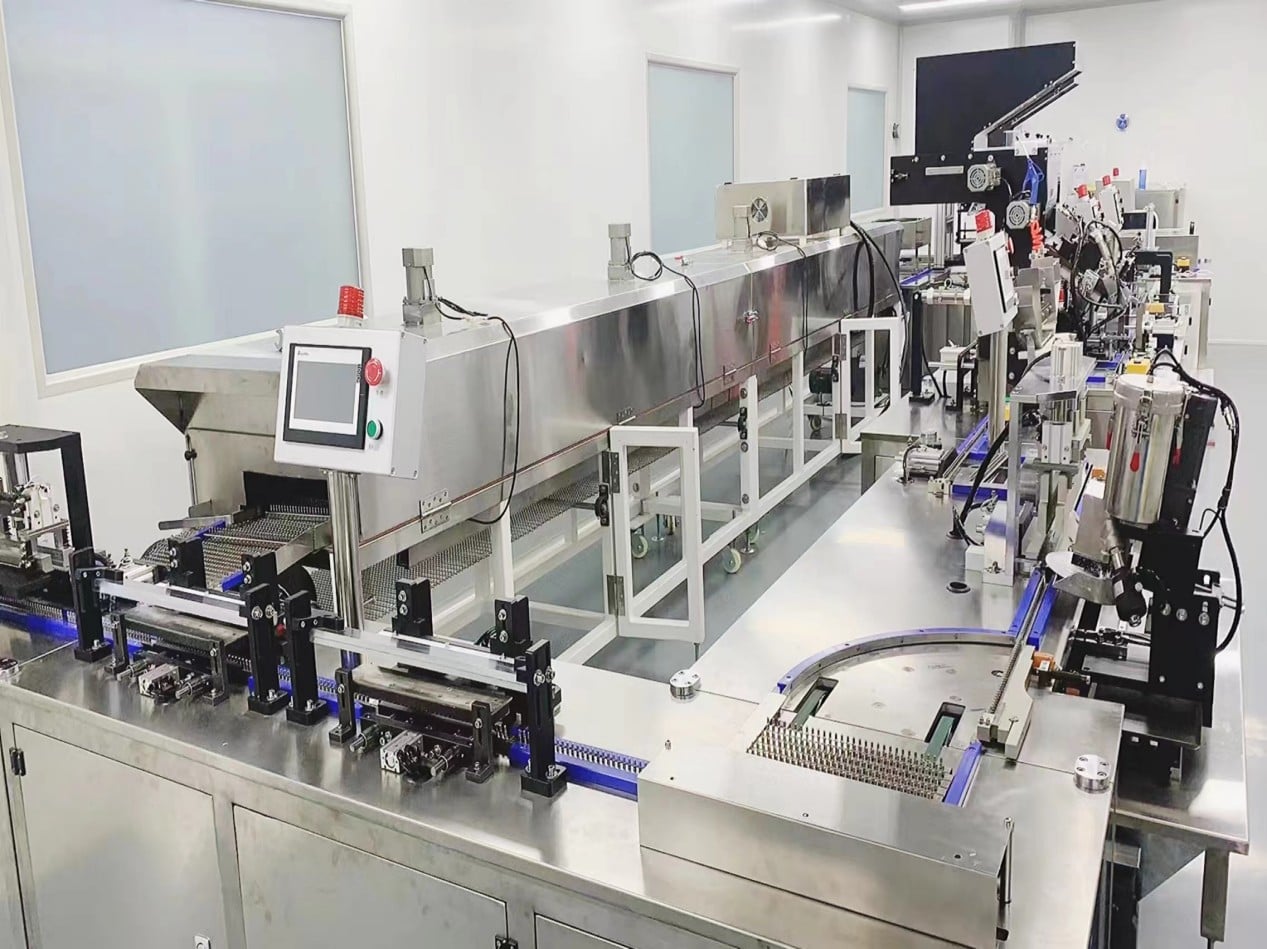
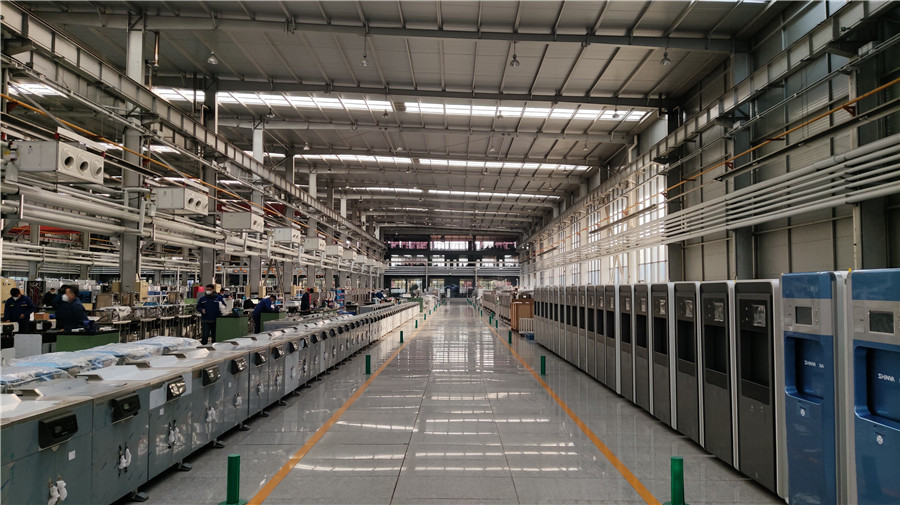
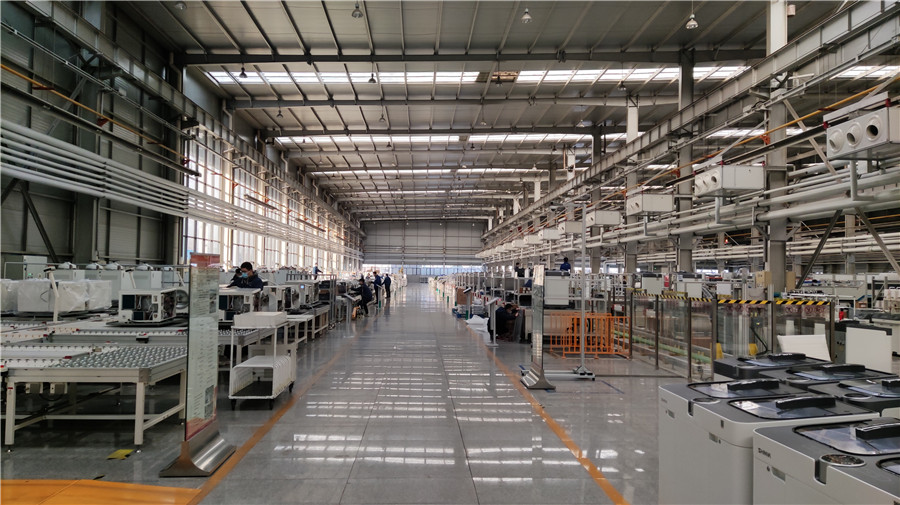
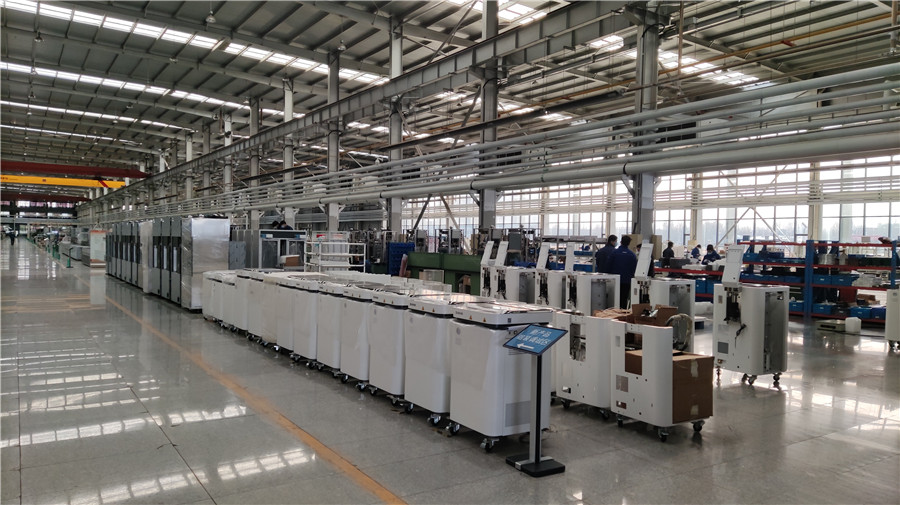
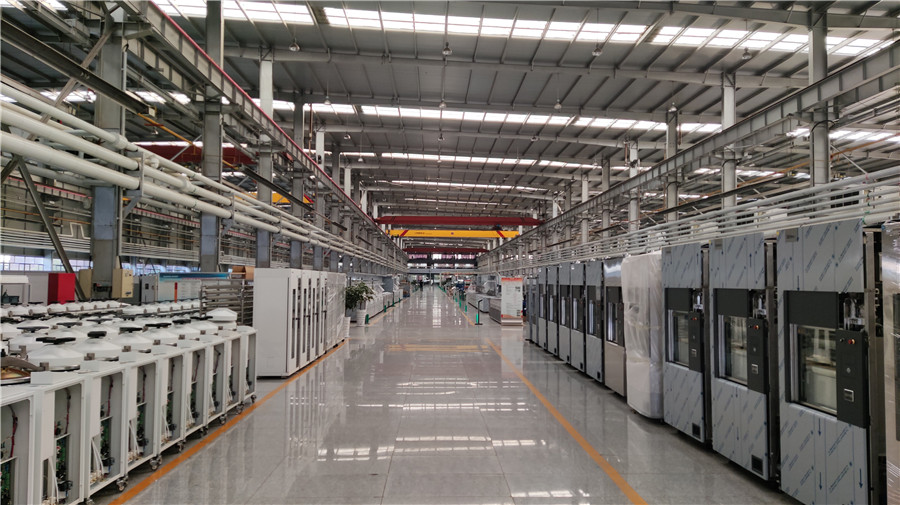
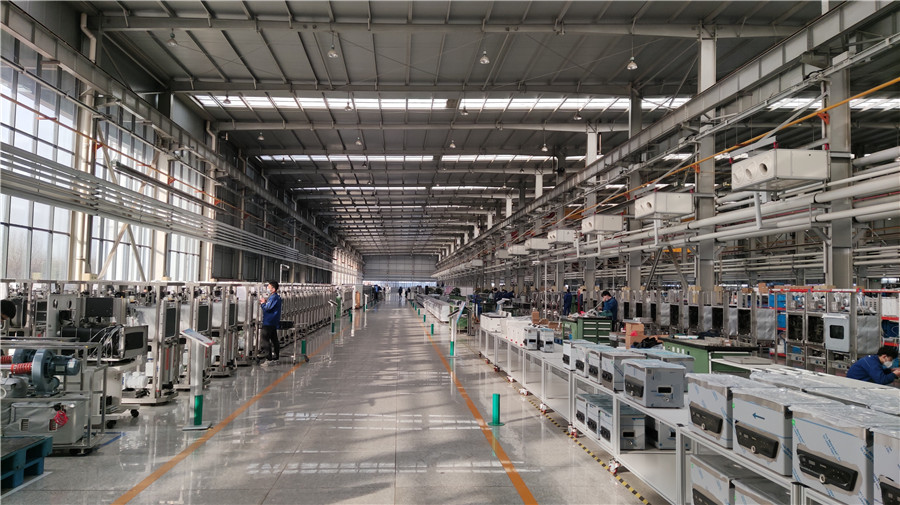
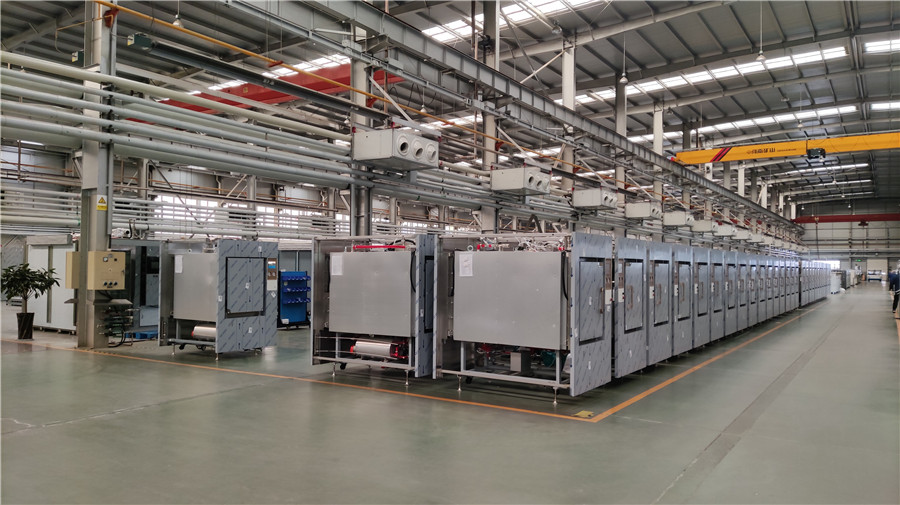
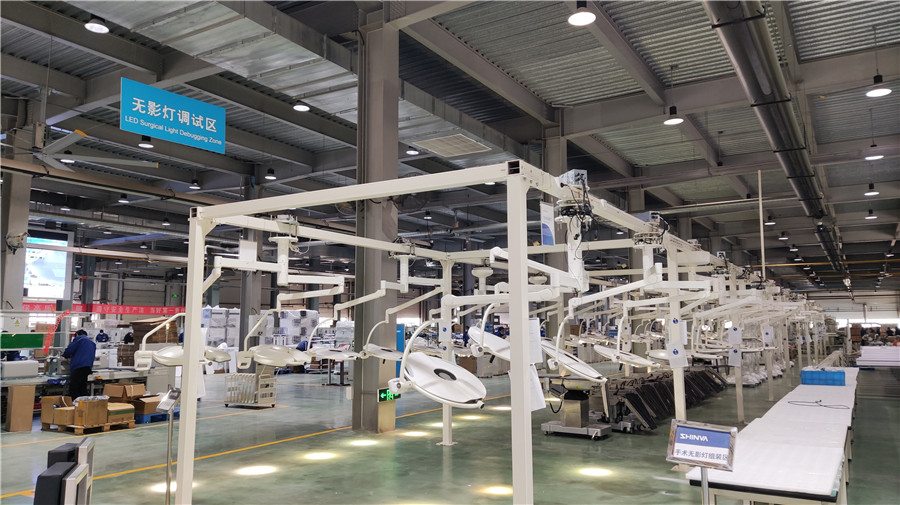
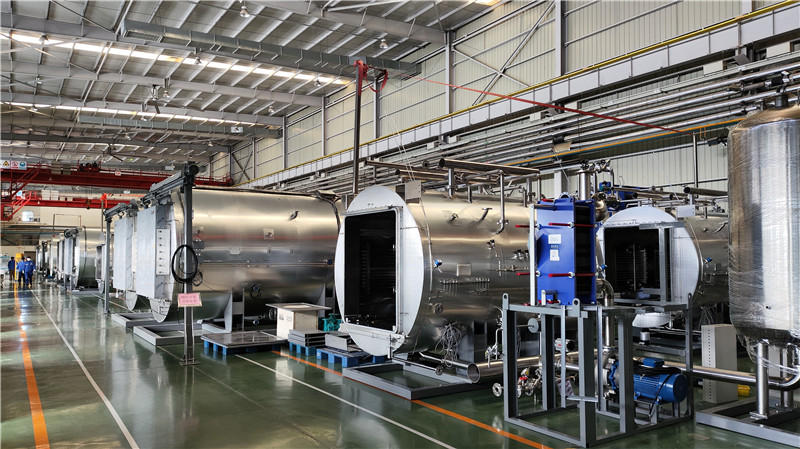
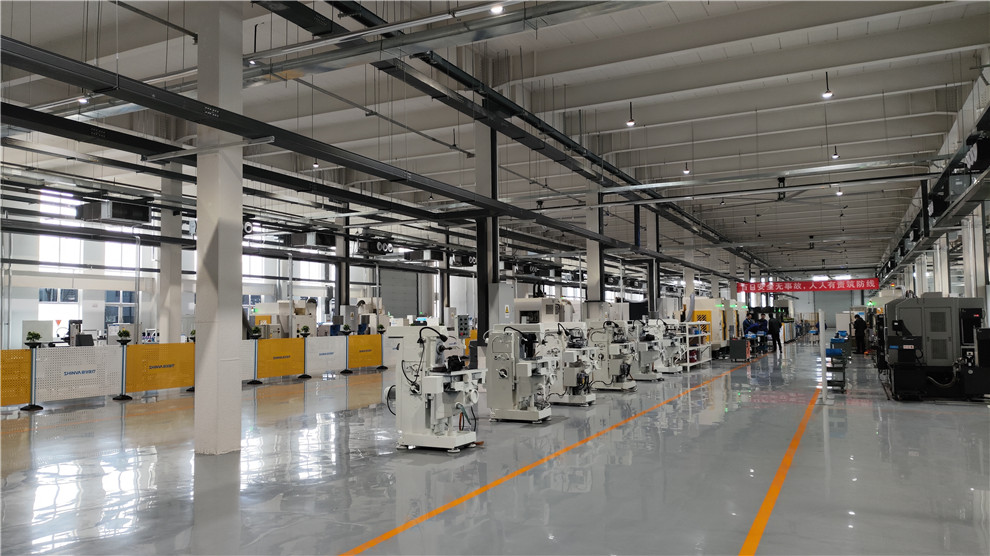
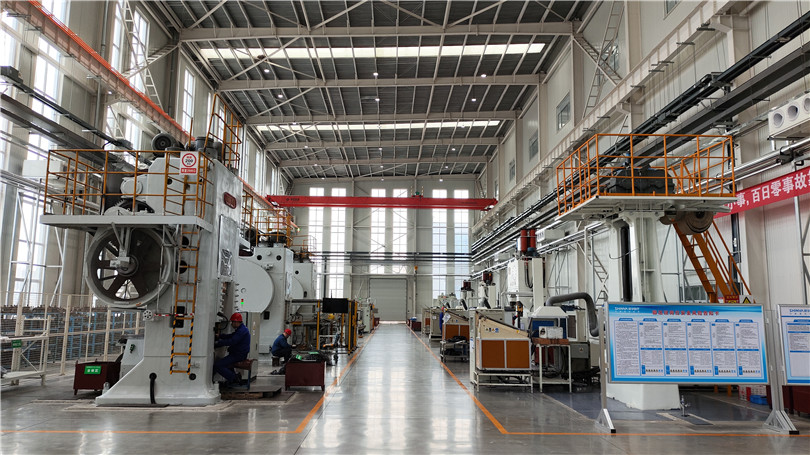
Inside Qingdao MDV Medical's advanced production environment, showing our focus on quality control and manufacturing safety.
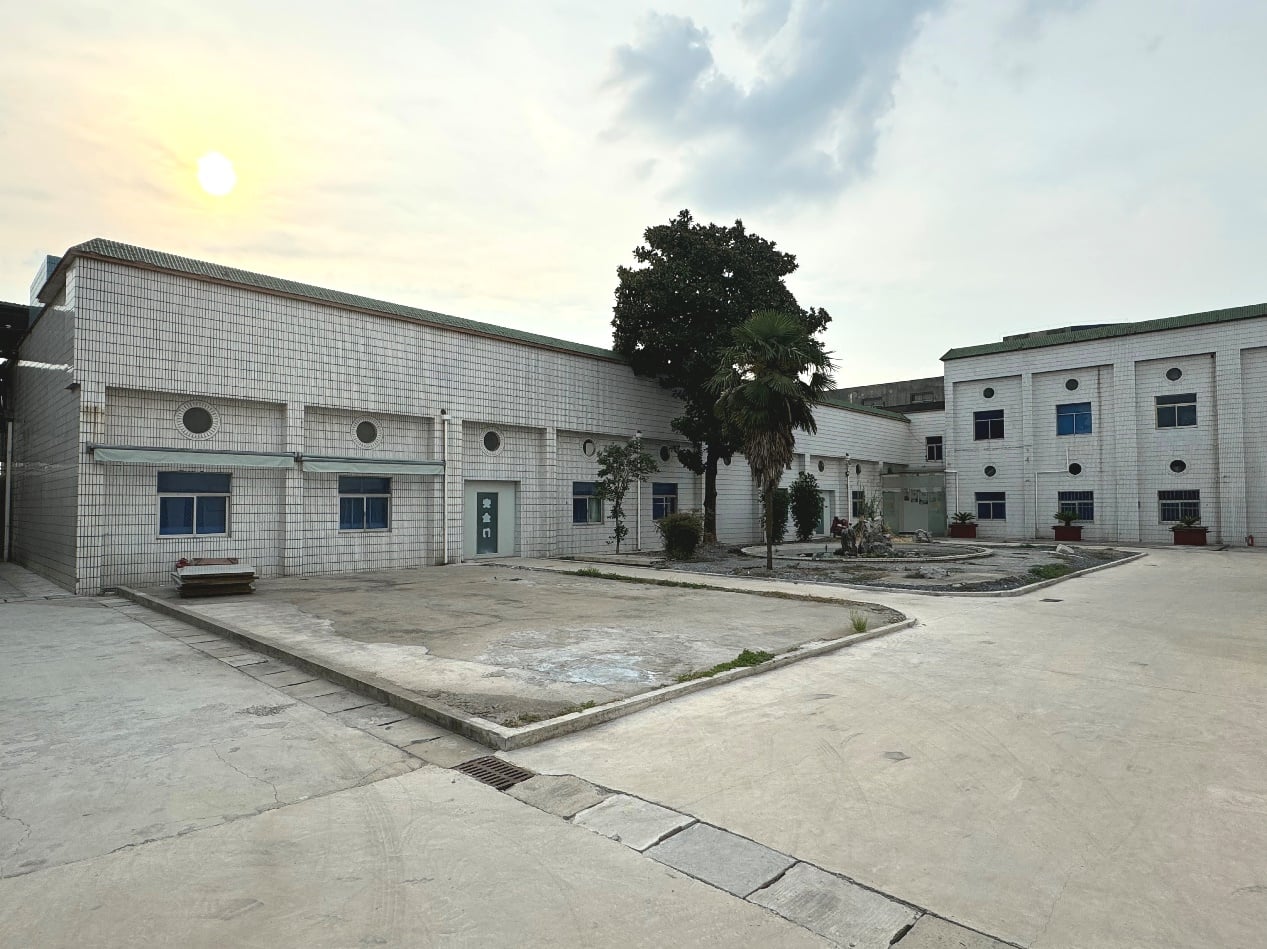
The company spans 6,600 sqm, with 4,700 sqm of construction area. The production area is 2,300 sqm, including a 1,500 sqm cleanroom and a 200 sqm quality inspection zone. It also features well-designed raw material, finished product, and sample storage facilities.
Our products are ISO 13485 certified, ensuring compliance with international medical device standards. Some also hold CE certification, meeting European regulatory requirements. These certifications reflect our rigorous processes and position us as a trusted partner, delivering safe and reliable products for global healthcare.
Qingdao MDV Medical Appliances Co., Ltd. has a 50-person team divided into production, quality control, and support units. This structure ensures efficient, high-quality manufacturing and compliance with global medical standards.
Always taking the tenet of creating high-quality medical equipment, caring for life and health, and providing customers with first-class products and service, our company have been constantly upgrading our existing products and developing new products.
Technical and regulatory answers to common procurement questions from healthcare administrators and clinical engineers.
Explore our specialized surgical instruments, veterinary diagnostics, and patient rehabilitation technologies.



 MDV Medical